YXYSteel information
Steel Plate Machining — Drilling, Milling & Boring
Drilling, tapping and thread milling, face and shoulder milling, rough and fine boring — machined after profiling, on the same datum as the cut edge, so the part reaches your fixture ready to weld.
Why wear plate machines differently
Hardness is only half of it. Abrasion-resistant plate also work-hardens under a dull edge and conducts heat badly, so a drill that survives mild steel will burn up here. Three rules cover most of it: keep the tool sharp, keep the chip leaving the hole, and keep the coolant where the cut is.
The parameters below are the ones we run for NM360–NM500. They are a starting point for quoting; the machine, the holder and the batch all move them.
Drilling
Solid carbide for small diameters, replaceable-blade drills from about Φ20 up. Short, stiff tools out-perform long ones — if the drawing allows a shorter drill, take it.
| Hole | NM360 | NM400 | NM450 | NM500 |
|---|---|---|---|---|
| Φ5 · solid carbide | 2500 / 250 | 2300 / 178 | 1910 / 152 | 1592 / 127 |
| Φ10 · solid carbide | 1270 / 127 | 1120 / 90 | 960 / 75 | 800 / 64 |
| Φ20 · replaceable blade | 1200 / 120 | 1100 / 90 | 950 / 75 | 800 / 65 |
| Φ25 · replaceable blade | 950 / 95 | 900 / 70 | 750 / 60 | 640 / 50 |
| Φ30 · replaceable blade | 800 / 80 | 750 / 60 | 650 / 50 | 550 / 40 |
Coolant: 8–10% emulsion, delivered through the tool where possible.
Chip evacuation decides the hole. Once the chip stops leaving, the flutes pack, the torque climbs and the drill breaks — usually on the last hole of a batch. If a hole starts oversized or undersized, check coolant flow and the filter before touching the speed.
Tapping or thread milling
Both work on NM360. Above M15, or from NM400 upward, we thread-mill: the cutter is smaller than the hole, there is no tap to snap in a hardened plate, and the thread can be corrected on the same setup.
| Grade | Cutting speed (m/min) | Feed per tooth (mm/z) |
|---|---|---|
| NM360 | 120 | 0.06 |
| NM400 | 110 | 0.06 |
| NM450 | 90 | 0.06 |
| NM500 | 80 | 0.06 |
Tapping NM360 with HSS taps runs at about 4 m/min and suits short batches only.
Milling
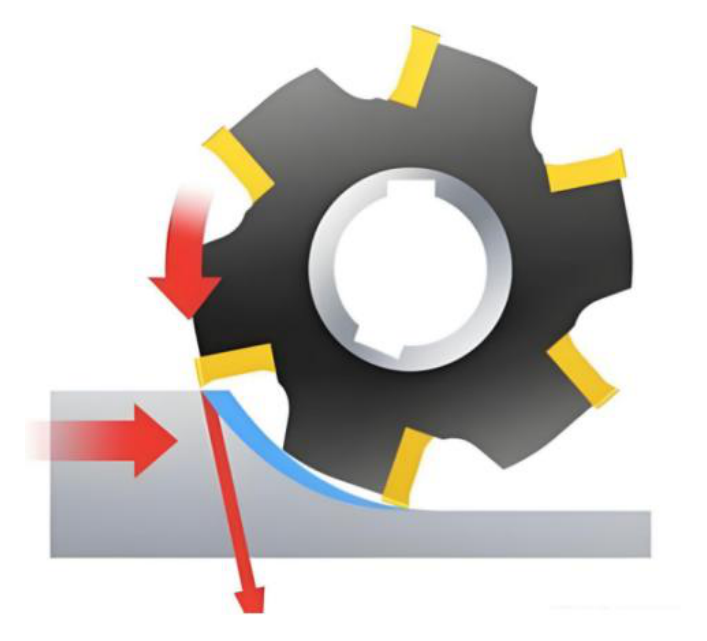
Face milling for surfaces and steps, shoulder milling for edges and grooves. We mill in climb mode on wear plate: the tooth enters at full chip thickness, which keeps rubbing — and work hardening — to a minimum. Conventional milling is reserved for thin walls where the vibration matters more than tool life.
| Grade | Speed | Feed | Removal |
|---|---|---|---|
| NM360 | 100 | 0.12 | ≤13.76 |
| NM400 | 100 | 0.12 | ≤13.76 |
| NM450 | 80 | 0.12 | ≤11.46 |
| NM500 | 80 | 0.10 | ≤10.32 |
| Grade | Speed | Feed | Removal |
|---|---|---|---|
| NM360 | 100 | 0.12 | ≤3.67 |
| NM400 | 100 | 0.12 | ≤3.67 |
| NM450 | 80 | 0.12 | ≤3.36 |
| NM500 | 80 | 0.10 | ≤3.36 |
Boring
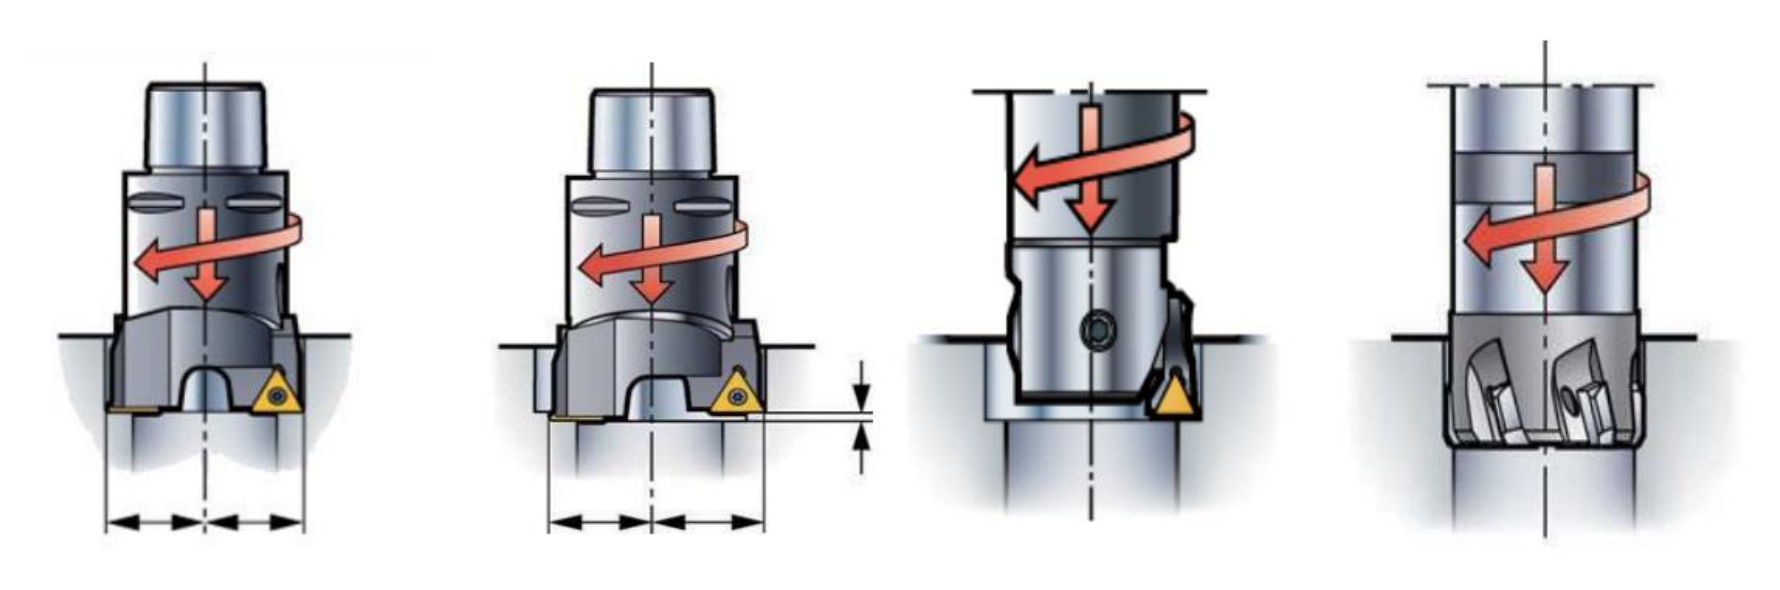
Rough boring takes the stock out, fine boring sets the size and the surface. Two passes, two tools, one bore that a pin will actually enter.
| Grade | Rough | Fine |
|---|---|---|
| NM360 | 100 / 0.15 / ≤25 | 120 / 0.08 / ≤1.25 |
| NM400 | 100 / 0.15 / ≤25 | 120 / 0.08 / ≤1.21 |
| NM450 | 90 / 0.15 / ≤21.88 | 120 / 0.08 / ≤1.33 |
| NM500 | 80 / 0.15 / ≤21.88 | 120 / 0.08 / ≤1.33 |
Clamping, coolant, and the two things that ruin a hole
Vibration and heat. Vibration comes from overhang and poor clamping — reduce the drill overhang, stiffen the fixture, drop the speed. Heat comes from coolant that never reaches the cutting edge: check flow, clean the filter, clear the coolant holes in the tool.
Parts are measured against the drawing before they leave, and the inspection record travels with the certificate.
Questions we get before the PO
Can you drill through 100 mm wear plate?
Yes, with replaceable-blade drills and a stepped program. Send the hole size and the tolerance band — deep holes are quoted with a pecking cycle.
Do you machine after cutting or before?
After. Profiling first means the hole pattern is drilled from the finished edge, not from a mill edge that gets cut away.
What tolerance can you hold on a bore?
Fine boring is the sizing pass; the band depends on diameter and depth. Give us the fit and we quote the boring allowance with it.
Can one order cover cutting, drilling and welding?
Yes — that is the reason the three sit in one plant. One drawing, one datum, one certificate.
Need a plate solution?
Cut, machined, welded and surface-prepared under one roof in Rizhao.