Fabrication bay
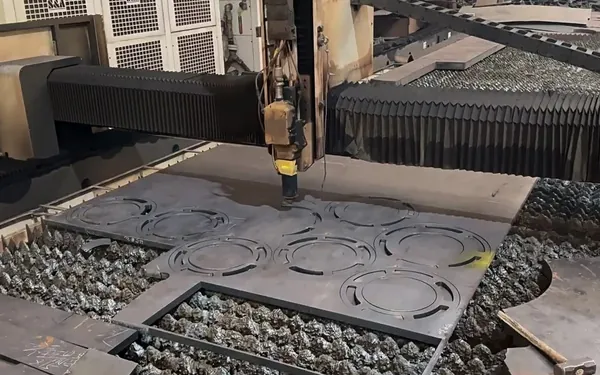
Multi-Head CNC Flame Cutting Line
Gantry flame-cutting line with a 16 m × 4 m envelope and up to four torch heads, cutting carbon and low-alloy plate from 6 mm to 300 mm with controlled preheating and slow cooling.
YXYSteel information
Processing · Medium & Heavy Plate
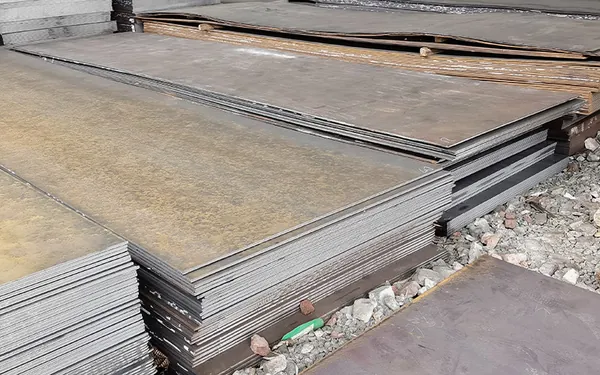
From 6 mm plate to 300 mm blocks, we cut, bevel and profile medium and heavy steel plate on multi-head CNC thermal-cutting lines and heavy machining centres, then deliver parts that fit the drawing the first time.
Cutting & Profiling Scope
Each part is cut on the process that matches its thickness, edge quality and the welding step that follows.
Gantry flame-cutting line with a 16 m × 4 m envelope and up to four torch heads, cutting carbon and low-alloy plate from 6 mm to 300 mm with controlled preheating and slow cooling.
Double-sided edge milling and beveling (V, Y and X bevels) plus heavy countersunk drilling, so parts arrive ready for automatic or robotic welding.
Nested profile parts, ring plates, gussets and replacement liners cut to your drawing — with a documented dimensional inspection report.
Crane-served bays with 10–40 t lifting and vacuum spreaders, handling long plates and heavy blocks without surface damage.
Grade guide
Typical route per grade. The final process is confirmed against the drawing, grade, thickness and quantity of your enquiry.
| Grade | Standard | Typical thickness | Cutting process | Typical applications |
|---|---|---|---|---|
| Q235B | GB/T 3274 carbon structural steel | 6–200 mm | Flame · plasma · laser | Base plates, brackets, general structural parts |
| Q355B | GB/T 1591 low-alloy high-strength steel | 6–200 mm | Flame · plasma · laser | Fabricated frames, machine supports, heavy weldments |
| 45# | GB/T 699 carbon steel for machining | 6–300 mm | Flame cutting + machining | Shafts, couplings, bushings and machined blanks |
| Mn13 | GB/T 5680 high-manganese wear steel | 8–150 mm | Plasma / controlled flame | Crusher jaw plates, hammer heads, wear liners |
Mn13 work-hardening grades are cut with controlled heat input and no water quenching to protect the wear layer; tolerances are confirmed per drawing before production.