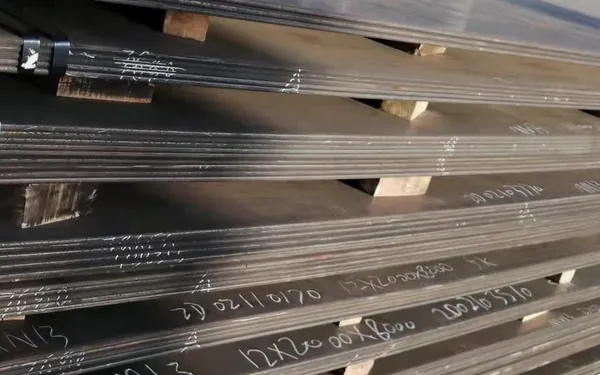
Thick plate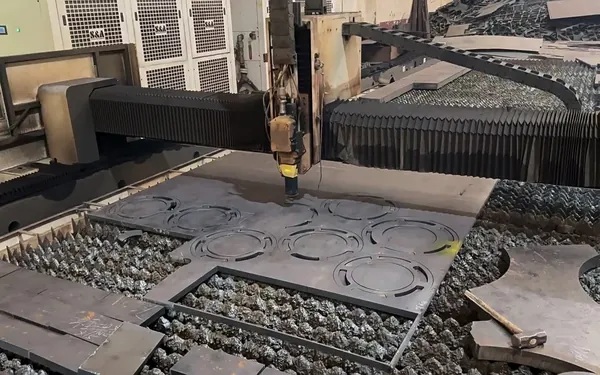
Multi-Head CNC Flame Cutting
Up to four oxy-fuel torch heads on a 16 m × 4 m gantry, cutting 20–300 mm carbon and low-alloy plate with controlled preheating and slow cooling.
YXYSteel information
Processing · CNC Thermal Cutting
Three thermal cutting processes on one cutting floor: multi-head CNC flame cutting for the thickest plate, high-definition plasma for fast carbon and stainless work, and 20,000 W CNC laser cutting for burr-free precision parts.
Process & Equipment
Flame, plasma and laser heads are matched to thickness, edge quality and the welding process that follows.
Up to four oxy-fuel torch heads on a 16 m × 4 m gantry, cutting 20–300 mm carbon and low-alloy plate with controlled preheating and slow cooling.
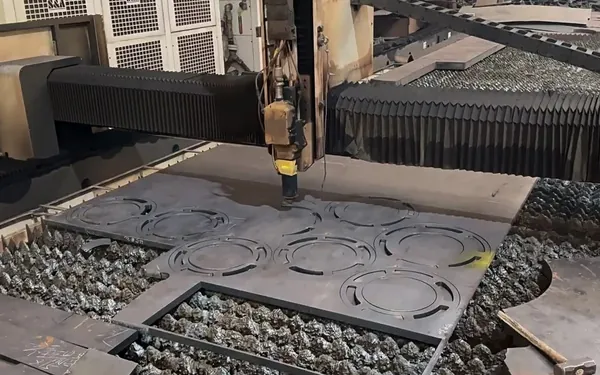
HD plasma for 6–80 mm carbon and stainless plate — fast cycles with a smooth, low-dross cut face that needs minimal secondary finishing.
Your CAD, DXF, DWG, PDF or scanned drawing is nested for material yield, then cut as profile parts, ring plates, gussets or replacement liners.
A 20,000 W laser on a 16 m × 4 m worktable cuts 6–60 mm plate with burr-free edges, tight tolerance and clean holes without secondary machining.
Process guide
Use this table as a process guide for your enquiry; the final route is confirmed against the drawing, grade and quantity.
| Process | Typical thickness | Achievable tolerance | Edge condition | Best suited to |
|---|---|---|---|---|
| CNC flame (oxy-fuel) | 20–300 mm | ±1.0 mm | Heat-affected, machinable | Thick plate, straight and profile cuts |
| HD plasma | 6–80 mm | ±0.5 mm | Smooth cut face, minimal dross | Carbon and stainless plate, fast cycles |
| CNC laser (20,000 W) | 6–60 mm | ±0.2 mm | Burr-free, tight tolerance | Precision parts, holes, complex nests |
| Bevel edge milling | 6–150 mm | ±0.5° bevel angle | V / Y / X bevel, weld-ready | Automatic and robotic welding preparation |
Accepted drawing formats: CAD (DWG/DXF), PDF and scanned drawings with dimension callouts. Material certificates accompany the finished parts on request.